
STINCO is a specialist manufacturer of centrifugal cast copper alloy components for demanding machinery applications. Our components have been supplied to Japanese press manufacturers including AIDA and Komatsu, and to injection molding machine manufacturers including Toshiba Machine, now known as Shibaura Machine, UBE Machinery and Niigata Machinery. In Taiwan, our copper alloy components are used by machinery manufacturers including Chin Fong Machine and Chuan Lih Fa Machinery.
These applications involve equipment where component reliability, wear performance, dimensional control and production consistency directly affect machine uptime, maintenance requirements and long-term operating cost.
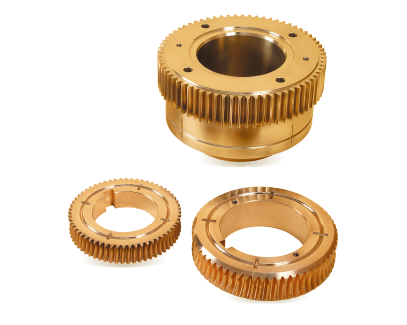
Advantages of Centrifugal Casting for Copper Alloy Machinery
Centrifugal casting is a manufacturing process in which molten copper alloy is poured into a rotating mold. The process is particularly suitable for hollow, cylindrical, ring-shaped or rotationally symmetrical components that require subsequent machining.
Centrifugal casting can be considered for copper alloy parts that must manage sliding contact, repeated loading, wear, lubrication conditions or corrosion exposure. It is commonly relevant to components such as bushings, sleeves, rings, bearing-related parts and other drawing-specific rotational components.
Advantages of STINCO in Copper Alloy Machine Parts Manufacturing
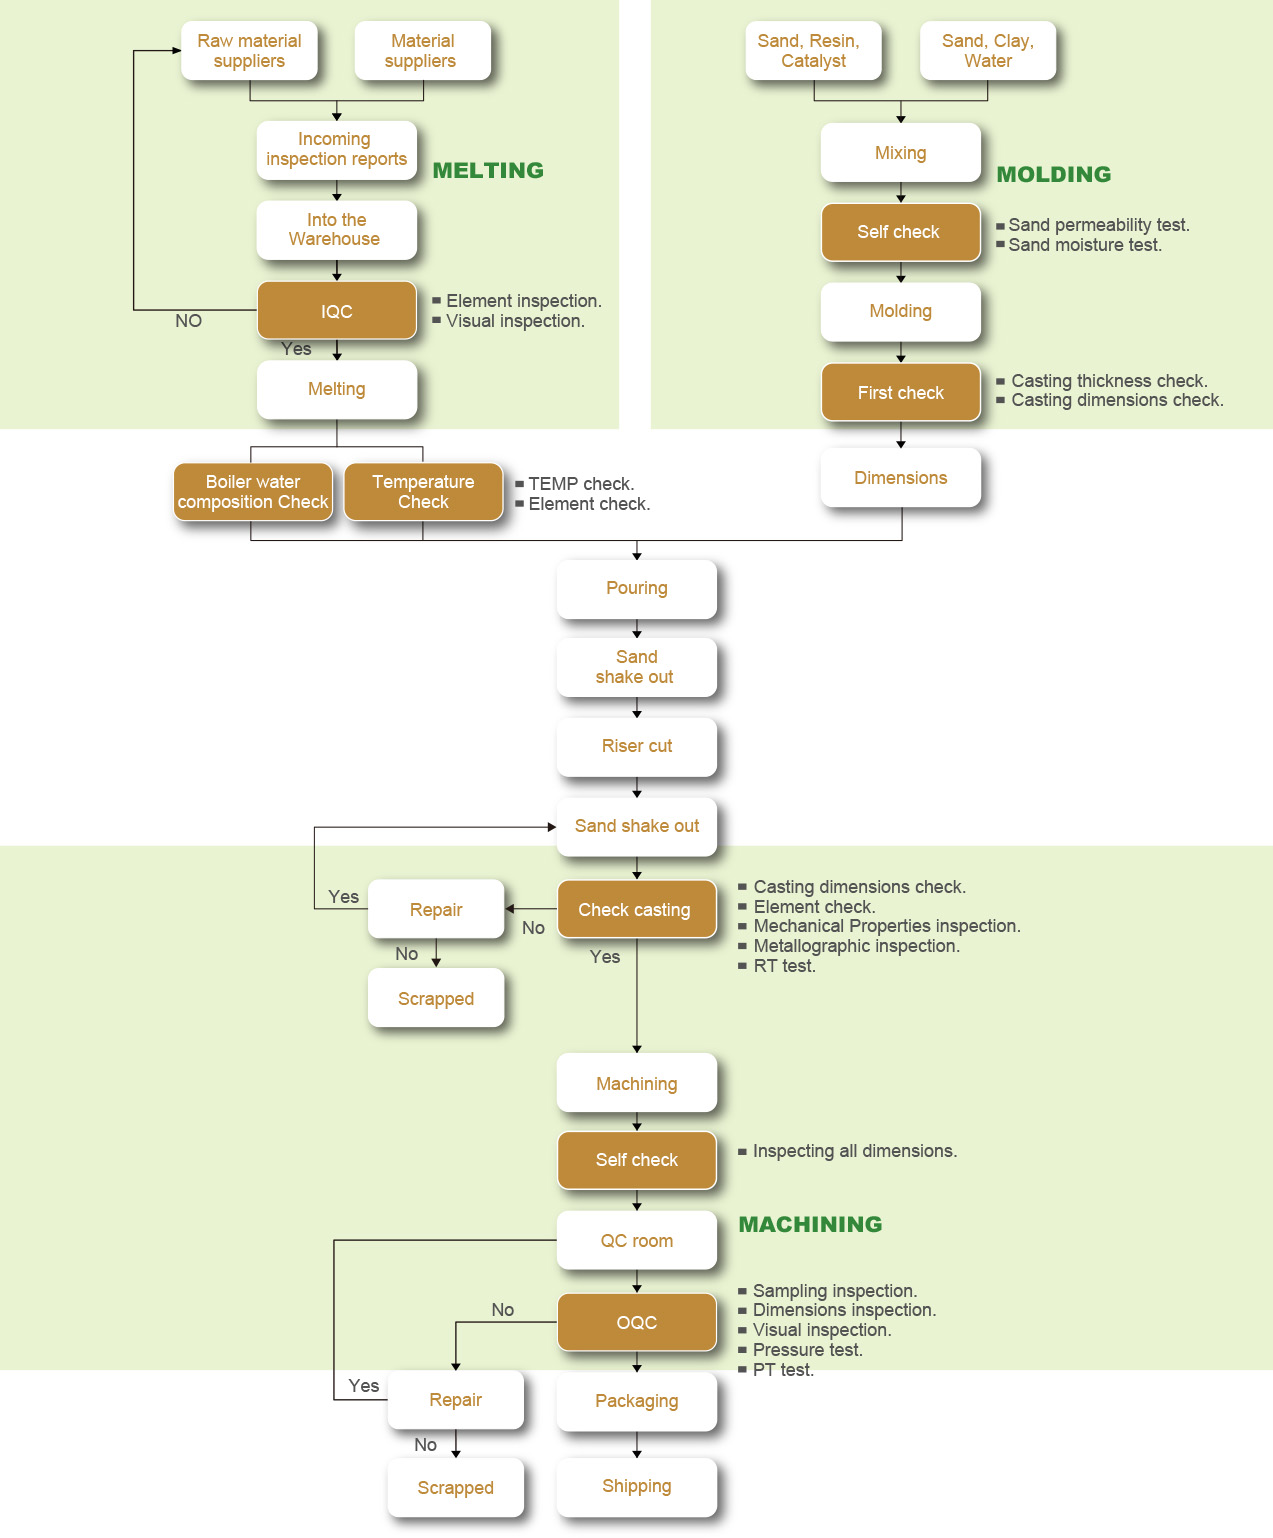
Choosing STINCO means choosing a controlled manufacturing and quality inspection process for centrifugal cast copper alloy components. Quality is managed from incoming raw materials through melting, molding, casting, machining and final release. This process helps reduce the risk of chemical variation, casting defects, dimensional deviations and machining problems reaching the customer.
STINCO reviews the component drawing, copper alloy grade, casting method, machining requirements and inspection plan before production. Our rigorous practices have earned the trust and recommendations of clients in Japan, Germany, and the United States.
Quality Control
| Quality control stage | STINCO’s process and inspection focus |
|---|---|
| Incoming material control | Raw materials are sourced from material suppliers and reviewed against supplier inspection reports. Incoming materials undergo composition and visual checks before entering production. |
| Melting control | Molten copper alloy is checked for chemical composition and temperature before pouring. This helps maintain the required alloy grade and casting conditions. |
| Molding control | Molding sand, resin, hardener and water are mixed under controlled conditions. Mold permeability and moisture are checked before molding. |
| First casting inspection | Initial castings are checked for casting thickness and key dimensions before continuing production. |
| Casting inspection | After pouring, cleaning and gate removal, castings may be inspected for dimensions, chemical composition, mechanical properties, metallographic condition and internal defects by radiographic testing, according to the agreed inspection plan. |
| Nonconforming casting control | Castings that do not meet the requirements are separated for repair or rejected. Only accepted castings proceed to machining. |
| Machining control | After machining, dimensional self-inspection is performed. Critical dimensions such as bores, faces and other drawing requirements are checked against the customer’s specifications. |
| Final inspection | The quality inspection room performs the agreed final checks, which may include sampling inspection, dimensional inspection, visual inspection, pressure testing and penetrant testing. |
| Release and delivery | Components are packaged and released for shipment only after the required inspections have been completed and accepted. |
Equipment & Capabilities
Which Copper Alloys Are Used for Press and Injection Molding Machinery?
Common copper alloy choices for machinery components include:
| Copper alloy family | Typical UNS grades | Typical machinery applications | Why it may be selected |
|---|---|---|---|
| Aluminum bronze | C95400, C95500 | Bushings, sleeves, guide components, wear rings and other high-load parts | High strength, wear resistance and good corrosion resistance |
| Nickel aluminum bronze | C95800 | Heavy-duty bushings, sleeves, wear components and selected rotating parts | High strength and resistance to wear and corrosion |
| Tin bronze | C90700, C93200 | Bearings, bushings, sleeves, gears and sliding components | Good bearing performance, machinability and compatibility with mating shafts |
| Leaded tin bronze | C93200 and other customer-specified grades | Bushings, bearing components and parts requiring conformability and machinability | Useful for selected bearing applications, subject to customer and environmental requirements |
| Manganese bronze | C86300, C86400 | Heavy-duty bushings, wear components and mechanical parts | High strength and resistance to mechanical loading |
STINCO reviews customer drawings, operating conditions, and production requirements to evaluate the feasibility of centrifugal casting and identify the optimal copper alloy for each machinery component.